Turning and Milling a Cylinder with Internal Slots
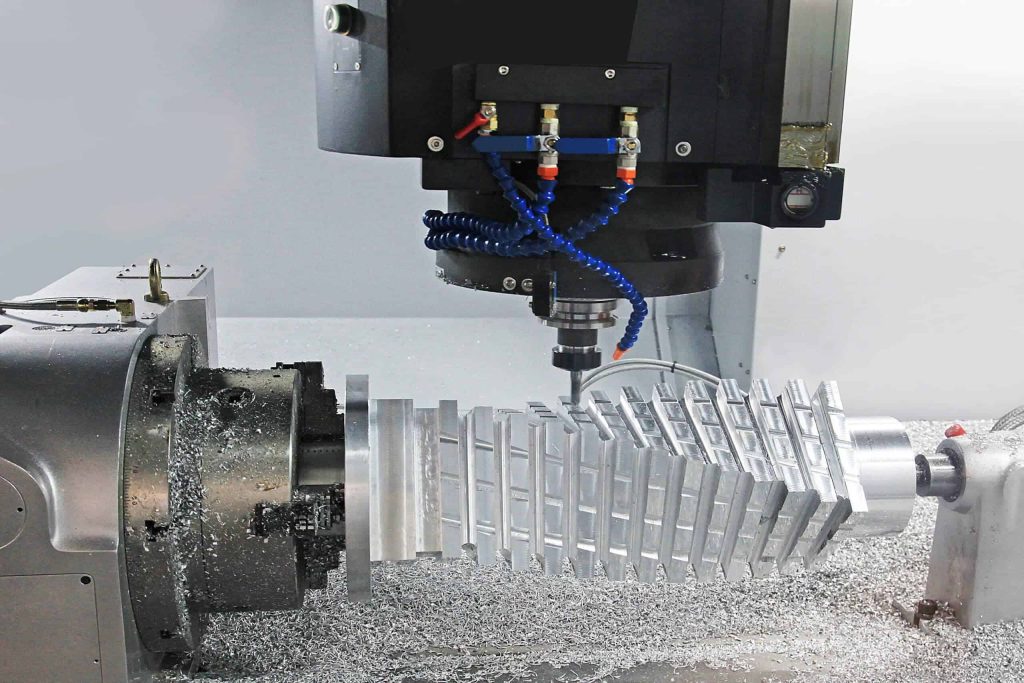
The operator identifies the non-circular internal profile and trapezoidal thread, then shows the turning and milling setups used on the same part.
Chapters
Selected chapter: Cylinder overview
Engineering notes
Identify which internal features can share the turning datum. Verify tool clearance and inspection access for the slots and thread before choosing the final setup.
Related engineering knowledge
Related manufacturing services and materials
Transcript
This part went through programming, setup, turning and milling.
We milled this slot because the internal profile is irregular and not circular.
The thread and the inside of the part were milled too.
The thread has a trapezoidal profile, and the bore is not perfectly round.
We programmed the details and worked through the profile with a T-slot cutter.
First, we roughed out the shape on the lathe.
Next, we used the machining center to work on the slots and the two flats.
We clamped the part for the first side, then reclamped it to reach the inside.
Then we finished the edges and cleared out the interior.
What would you quote for a part like this?