Clamping and Cutoff for a Multi-Sided Bracket
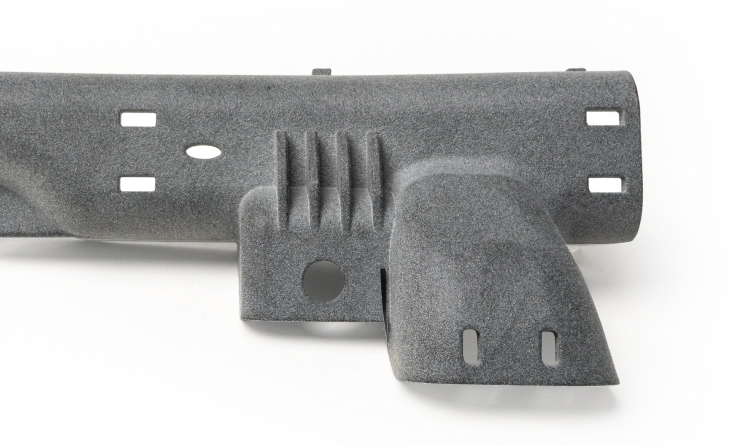
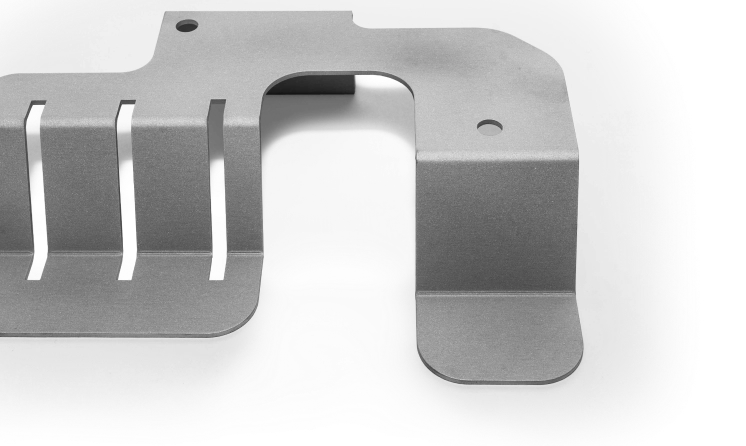
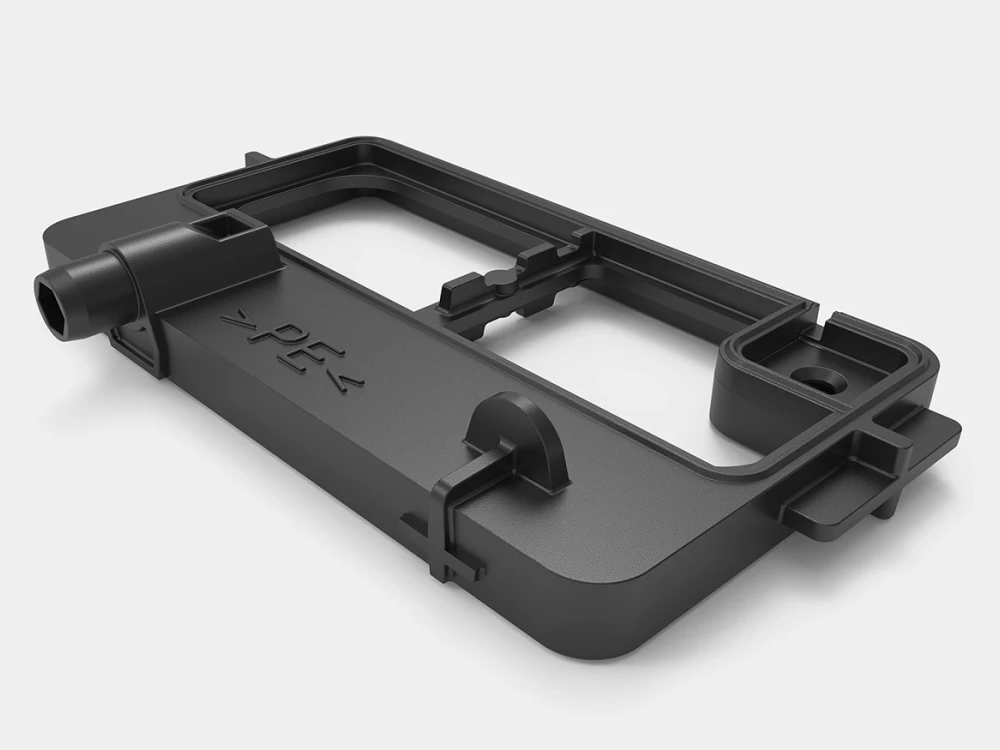
The operator shows the bracket, reorients the work in its fixture, mills a slot and cuts the part free. The remaining material supports the part until the cutoff step.
Chapters
Selected chapter: Part and setup
Engineering notes
Review which faces need to remain accessible and whether the remaining stock can support the part until cutoff. Clamping forces, dimensions and acceptance results are specific to the job.
Related engineering knowledge
Transcript
Machining and finishing averaged about an
hour per part.
We made ten parts on the machine behind
me.
A three-axis machine could do this, but
the setup would be more involved.
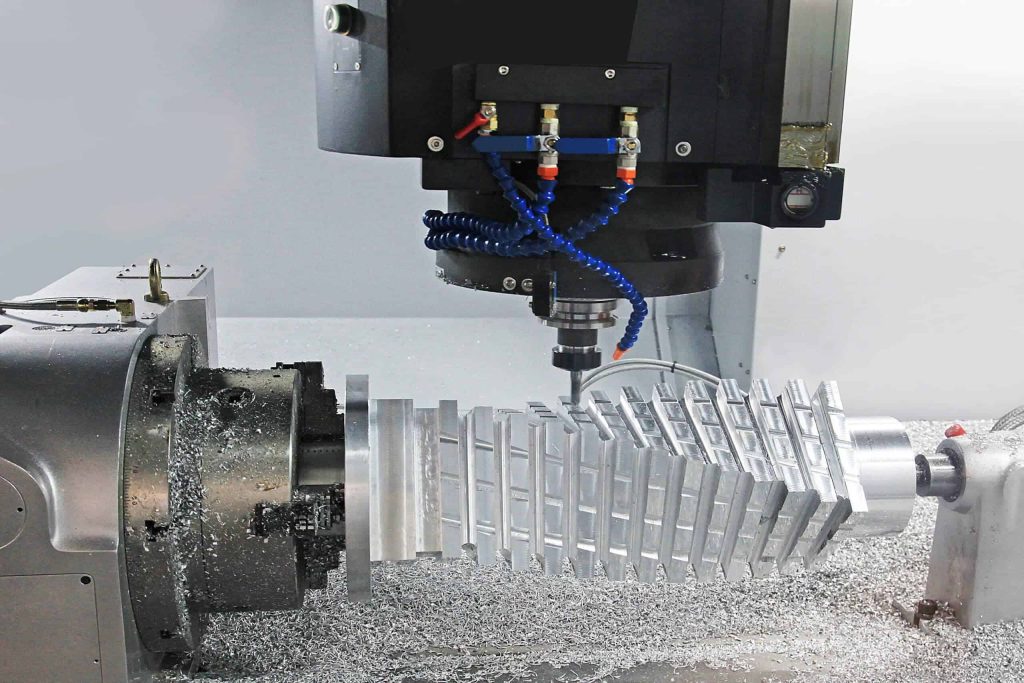
We used five axes for a simpler setup. The
three-axis machine was busy.
The five-axis setup uses more stock for
clamping.
Machine the rear clamping area, then turn
the part over.
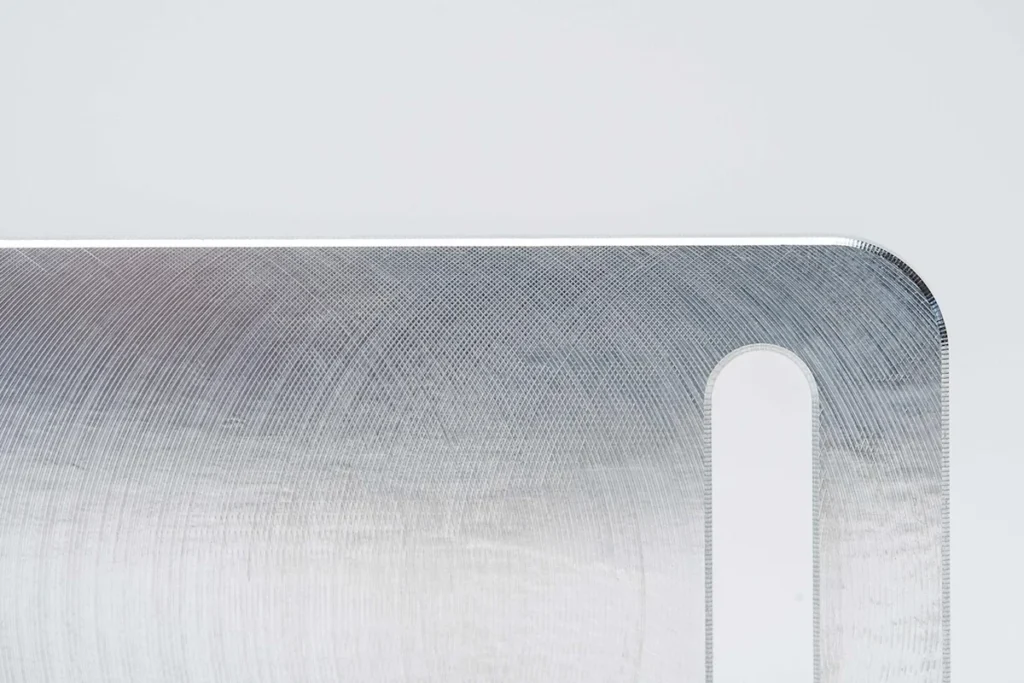
Face the side and mill the edges with a 2D
toolpath.
Index the part to reach the slot, then cut
the slot to fit.
Finish the slot, cut the edge and clean up
the features.
Finally, cut around the profile to
separate the part.
That finishes the job.
What would be a fair price per part?