Tool Access for a Deep-Pocket Enclosure
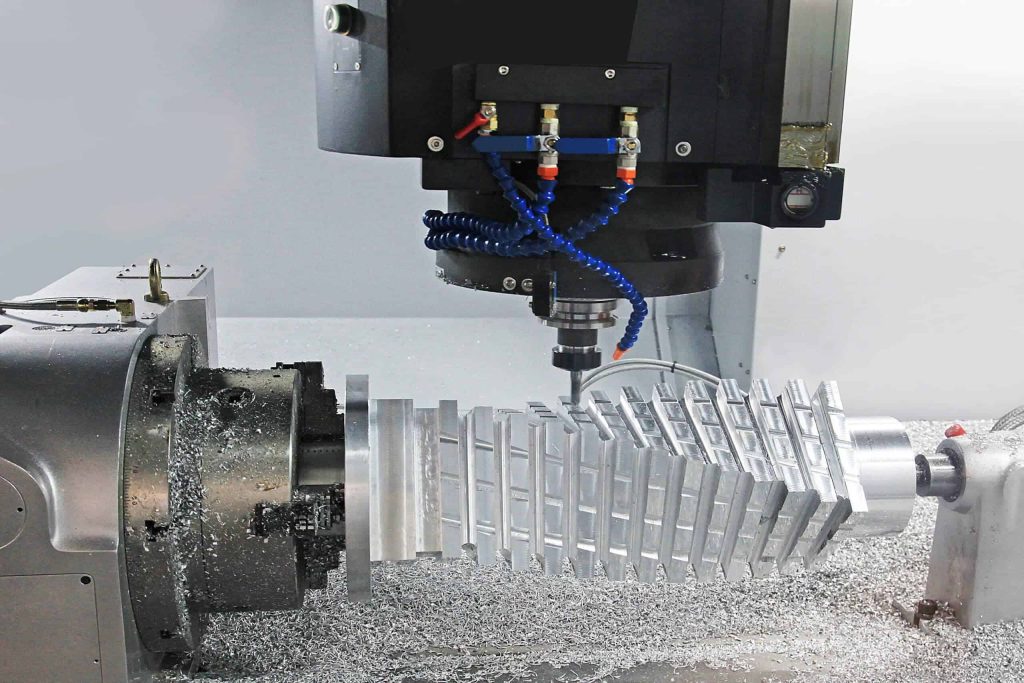
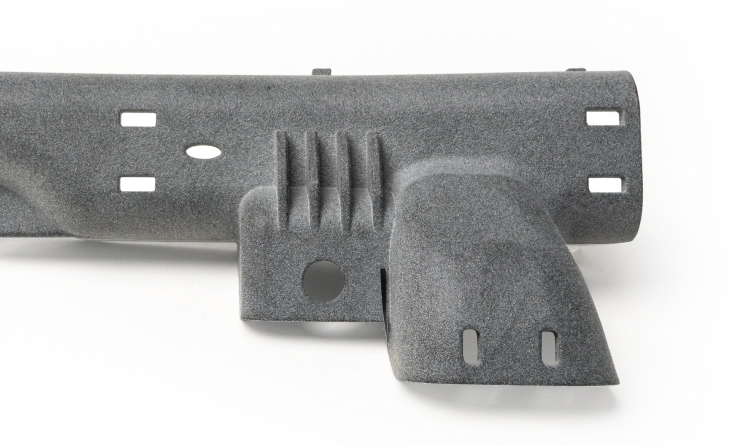
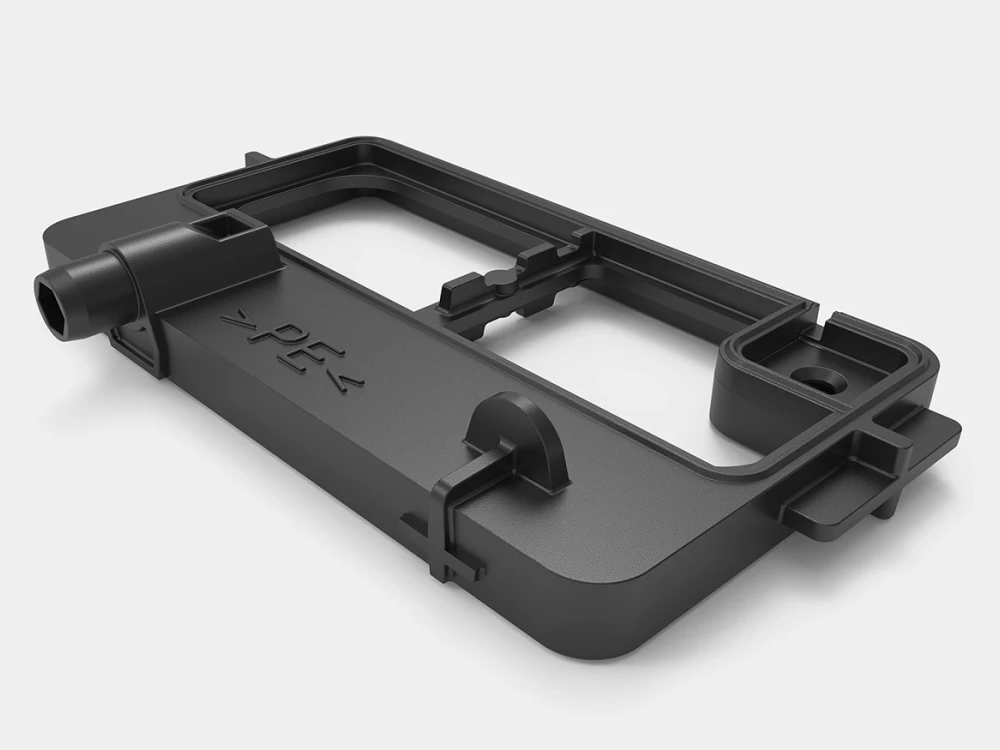
The operator presents a pocketed enclosure, describes the initial three-axis setup and shows the tool reaching into the pocket before pointing out side features.
Chapters
Selected chapter: Three-axis setup
Engineering notes
Check pocket depth, corner radii and tool clearance with the manufacturing team. Identify which side features need the enclosure to be reoriented.
Related engineering knowledge
Transcript
Stock for the job was 230 yuan. Ten pieces
took 80 hours.
There are three-axis and five-axis
operations to reach the different faces.
The inside was machined here. Start with a
three-axis setup.
Machine a clamping feature, then hold the
part at the base for the five-axis work.
Index to mill the five faces and the
curved corners.
Use simultaneous motion to finish the
sharp edges, then return to three axes.
The part is tall, so two aluminum blocks
support it while the interior is machined.
The opening is smaller than the interior.
The cutter has to reach under the lip.
The part can be damaged if the tool is not
used carefully.
We made ten parts. What do you think each
piece is worth?