Reclamping a Turned Cylinder for Off-Axis Features
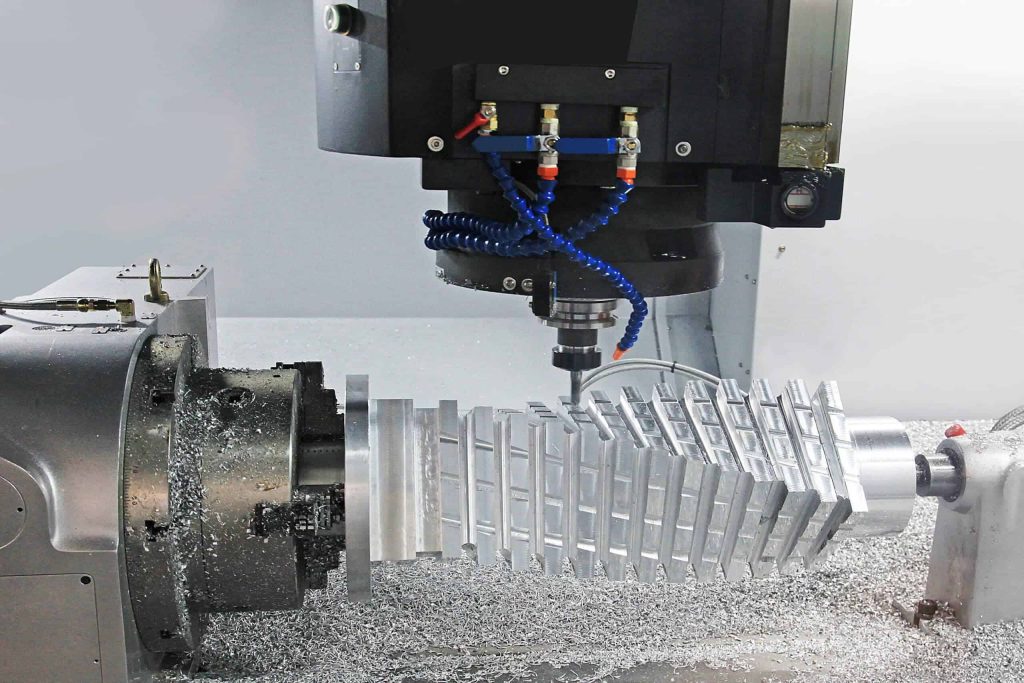
The clip follows a cylindrical workpiece through a lathe chuck and a second fixture. The operator shows how a different orientation provides access to features away from the turning axis.
Chapters
Selected chapter: Component overview
Engineering notes
Review which surfaces remain available for clamping after turning. Confirm the thread and hole requirements from the drawing.
Related engineering knowledge
Transcript
We made two pieces. Programming and
machining took a little over two shifts.
The top and bottom are angled.
Four holes are normal to the round
feature.
Start by turning the stock and leaving
material for clamping.
After the first five-axis operation,
reclamp it to machine the other side.
Machine the angled top, then the bottom.
Reposition the part in a second fixture to
reach the inside.
Grip the reserved clamping area to machine
the center feature.
Secure this section, then move to the
three-axis machine.
Drill the small holes. We made two parts.
What do you think of this job?