Rotary Workholding for a Cylindrical Housing
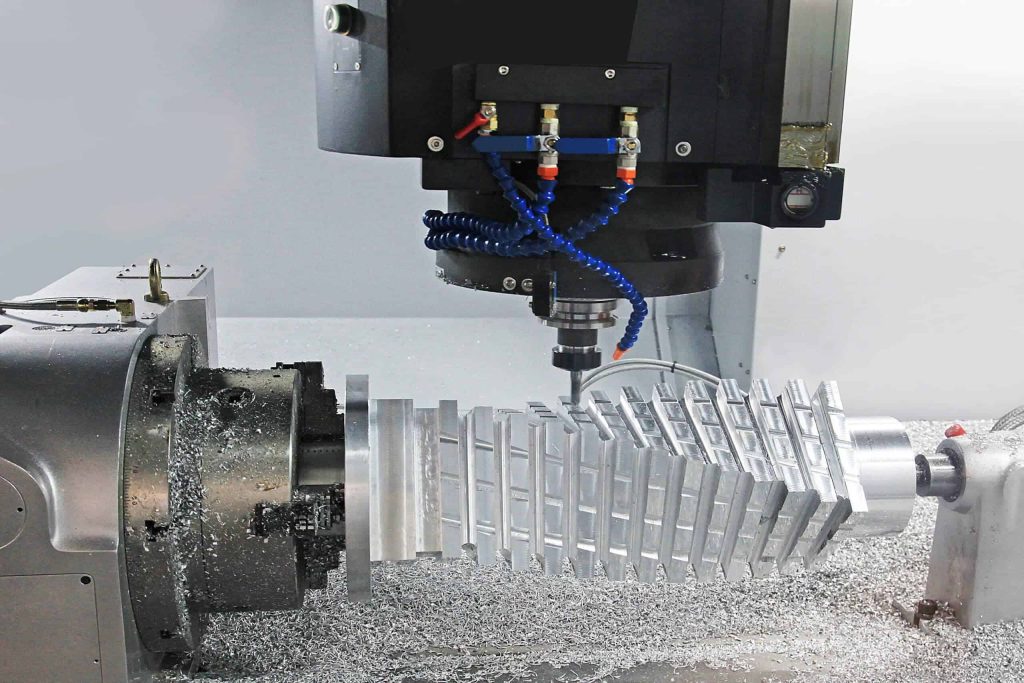
The operator shows a cylindrical housing in a chuck, then presents a supported machining setup and a rotary fixture that gives the tool access to side openings.
Chapters
Selected chapter: Housing overview
Engineering notes
Check how the housing is supported when the tool reaches side openings. Confirm the angular locations and reference features from the drawing.
Related engineering knowledge
Transcript
Programming and machining took 40 hours on
this job.
The parts need anodizing. This is the
machine we used.
Leave the stock long. Chuck it in the
lathe and turn the outside down to this
step.
Face the end and plunge the groove.
Turn the part around and face off the
excess stock.
Machine the end groove, then bore the
inside.
Make a support fixture with a stud through
the center.
Fit the cover plate, tighten the screws
and drill the top holes.
Use an extended tool to mill the three
lower notches.
Set up a rotary fixture with a draw rod
and a plate with four locating pins.
Orient the part, seat the pins in the four
holes and secure the fixture.
On the rotary axis, mill the top features
and openings.
There were five setups, and we made seven
pieces.
What do you think of the job? What would
you charge?