Vacuum Clamping and Slot Milling for a Finned Plate
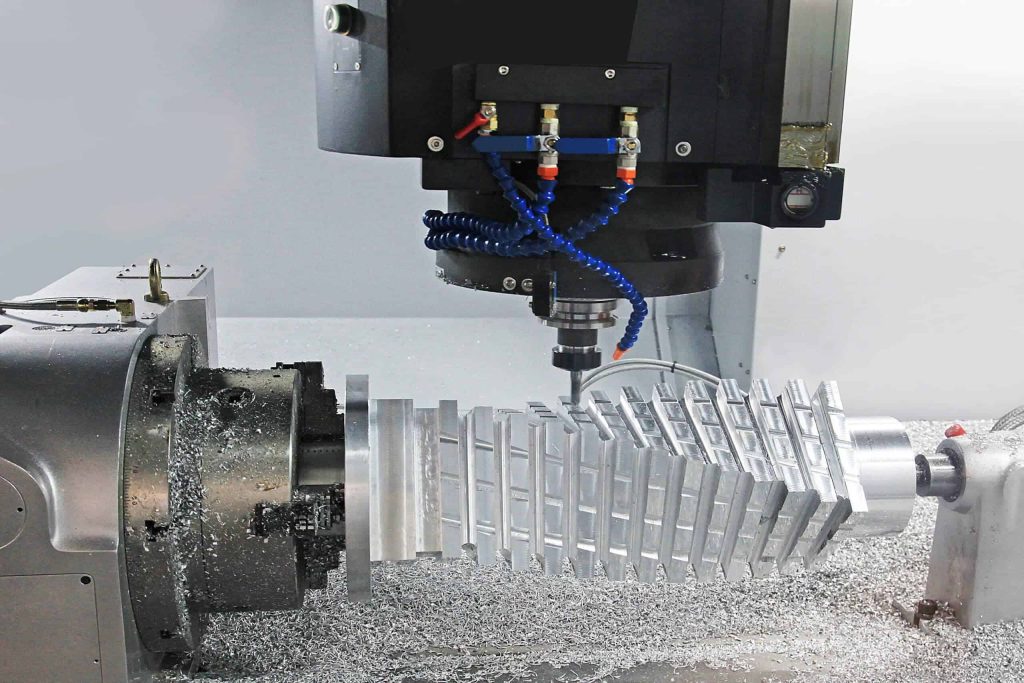
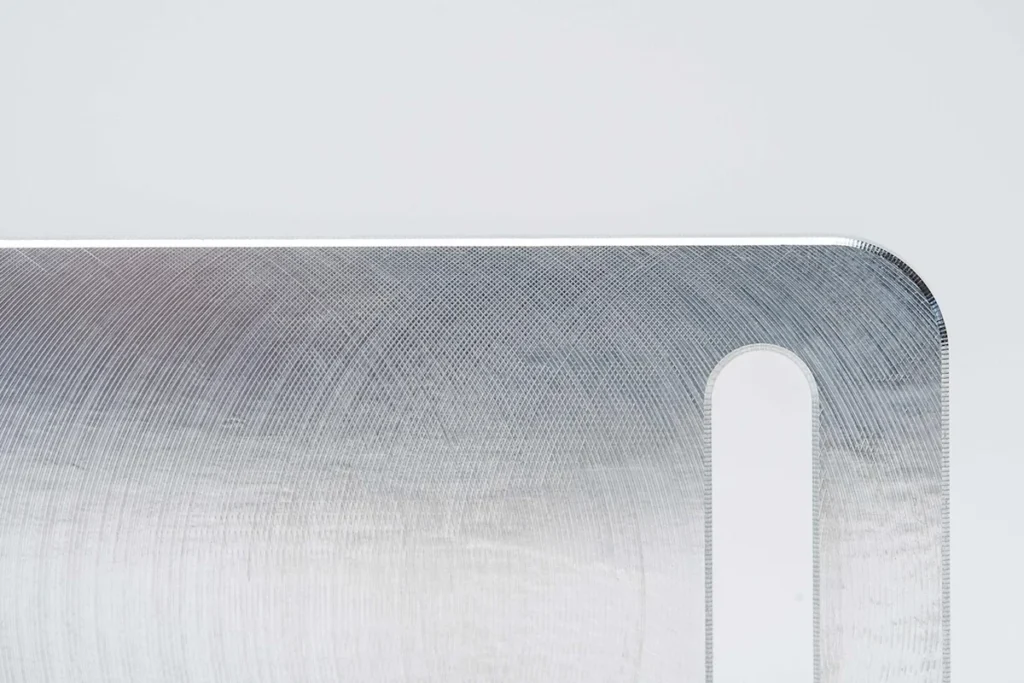
The operator seats a finned plate on a vacuum fixture and works on the narrow parallel slots. The clip shows the plate being held again when the operation moves to the other side.
Chapters
Selected chapter: Second clamping step
Engineering notes
Check which areas can maintain a seal while the slot pattern is machined. Confirm how the part is supported before releasing a flatness requirement.
Related engineering knowledge
Transcript
Stock was 130 yuan per part, and the job
needs anodizing.
We made 13 parts. Programming and
machining took four and a half shifts.
The small slots take the most time. They
run around this face.
Hold it on the vacuum chuck, face the
stock and clear the center.
Drill the holes and mill the outside
profile to size.
Mill the small slots and finish this face.
The part is no longer flat. Flip it over
for the other face.
Make a vacuum fixture to fit the machined
features, then add the seals.
Hold it on the fixture and face the other
side.
Mill these small slots, then machine the
stepped holes.
Both setups were on the three-axis
machine.
We made 13 parts. What would you charge
per piece?