Injection molding materials: resin selection checklist
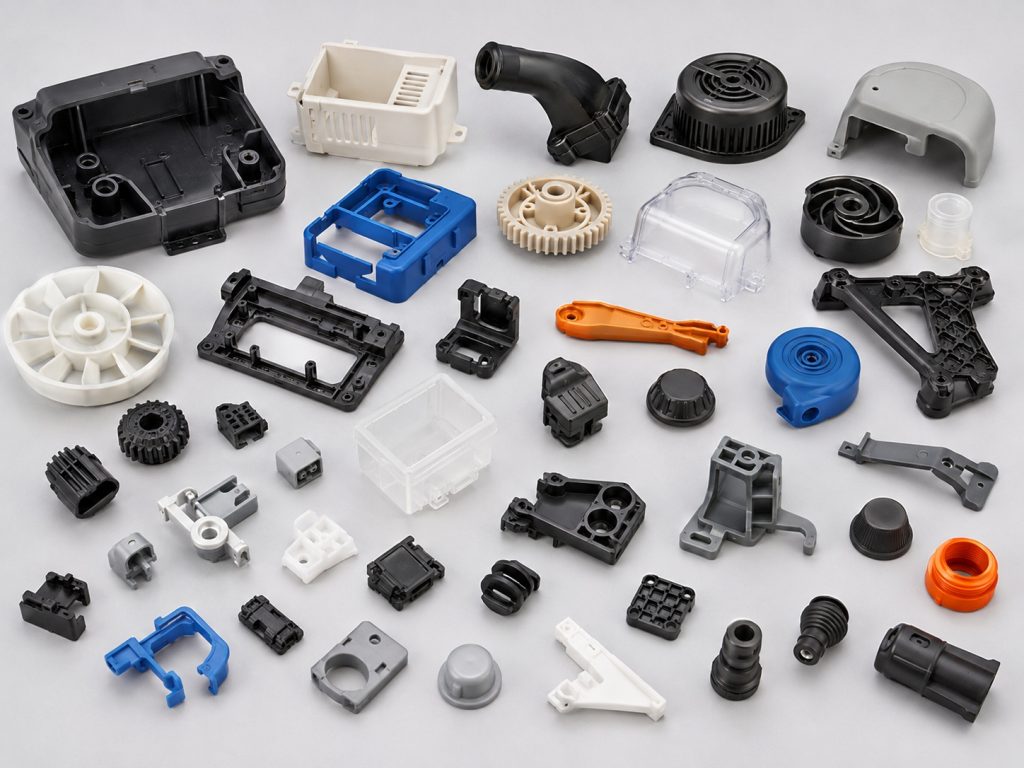
Choose the exact resin grade around part function, tooling, dimensional requirements and service conditions. This reference is a starting point for review, not a stock list or a guarantee of material availability.
Resin-family review checklist
Use the material designation with its supplied condition and a clear drawing. The notes below describe what to verify; they do not establish a universal tolerance, price, certification or performance level.
Open any resin to review its requirements. Keep multiple sections open to compare, then follow the material or process link for the next step.
ABS
Define the housing or part function, impact requirement, cosmetic texture and service exposure. Confirm the exact resin grade, color and any documentation requirements rather than treating all ABS grades as interchangeable.
Polypropylene (PP)
State whether the part needs flexibility, a repeated-motion feature, chemical exposure or a rigid interface. Provide the exact grade and geometry so shrinkage, warpage and the tooling approach can be reviewed together.
Polyamide 6 (PA6)
Specify the resin grade, reinforcement and the conditioning state used for dimensions and testing. Ask how moisture condition, fit and inspection will be controlled for the actual part instead of applying a generic tolerance to every nylon design.
PMMA / acrylic
For a clear or appearance-critical component, state optical or cosmetic expectations, surface references and allowable witness areas. Review the drawing, intended handling and service exposure with the selected grade before committing to tooling.
Polycarbonate (PC)
Identify the impact, transparency, temperature and assembly requirements that drive selection. Confirm the grade, finish and acceptance criteria for the component; an application name alone does not establish compliance or suitability.
POM / acetal
For a moving, locating or bearing interface, provide the mating material, loading, fit and inspection condition. Review the exact resin grade, geometry and dimensional requirements before assigning shrinkage allowances to the tool.
PEEK
State the service conditions, reinforcement, critical dimensions and required documentation. Review whether the selected grade, tooling and processing route can meet the part requirement; the family name is not a certification or a universal performance guarantee.
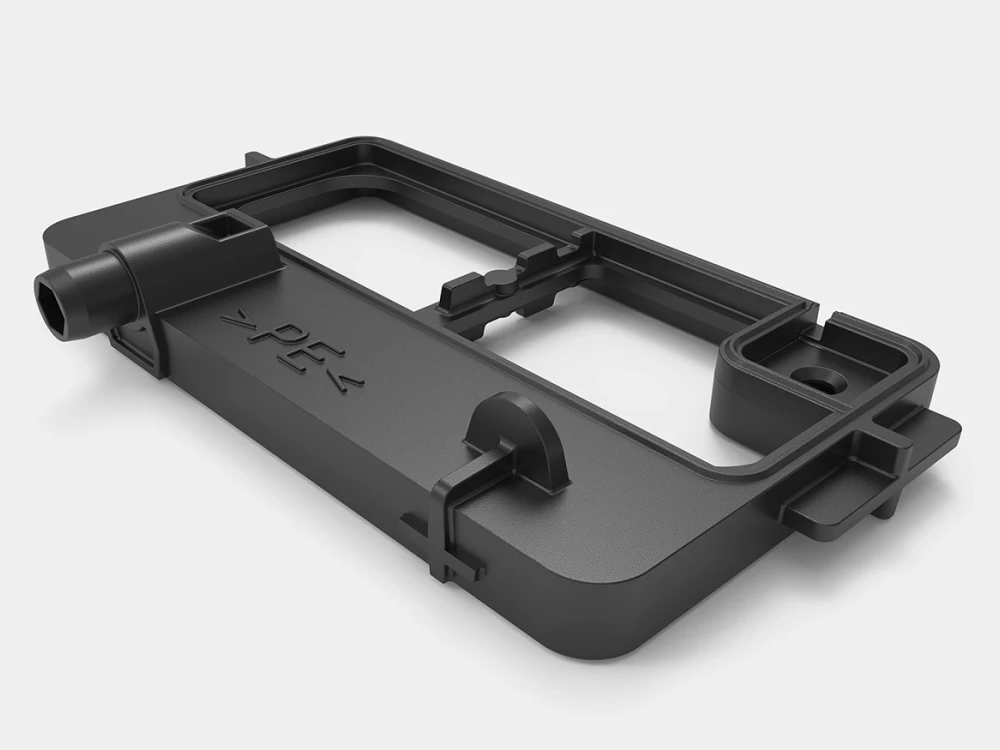
Polyethylene (PE)
Use the exact grade and density designation in the specification. Describe flexibility, contact conditions, service exposure and the intended assembly so that a general PE label does not conceal the choice between materially different grades.
PET
Confirm the exact grade, intended process and part function. Review dimensional stability, finish and any contact or regulatory requirements against supplier documentation and the actual component, not a generic catalogue tolerance.
PVC
Specify the formulation, intended application and the supplier-approved processing route. Confirm equipment compatibility, handling requirements and required product documentation with qualified specialists before treating the material as a manufacturing option.
HDPE
Identify the actual grade and the functional requirements for the part. Provide wall sections, joining or closure details, service exposure and inspection conditions so material selection and tool design can be reviewed as one decision.
LDPE
Describe the required flexibility, geometry and contact conditions. Confirm the grade and part acceptance criteria with the supplier; do not copy shrinkage or tolerance values from a different polyethylene grade or product form.
PTFE needs a separate process review
PTFE is not interchangeable with conventional melt-processable injection-molding resins. Confirm the material grade and an appropriate processing route before quoting the part. Do not apply the generic injection-molding shrinkage or tolerance values from another resin to PTFE.
Manufacturer reference: Daikin explains the processing distinction between PTFE and melt-processable fluoropolymers. This reference does not establish Debaolong equipment, stock availability or application approval.
What to send for engineering review
Identify the exact resin
Provide the manufacturer, grade, reinforcement, color and any approved alternatives. Confirm that required documentation applies to that grade and intended use.
Connect the material to tooling
Review wall sections, ribs, gates, ejection and cosmetic faces. Treat shrinkage allowances and dimensional acceptance as part-specific decisions, not catalogue constants.
State the inspection condition
Specify when and how dimensions and performance are checked, including any conditioning or assembly state relevant to the requirement.
Confirm before production
Agree material supply, process feasibility, sample approval and required evidence. Medical, food-contact, electrical or other regulated suitability needs its own documented assessment.